A compressor that cuts out 8 psi late can look like a minor maintenance issue until it creates pressure alarms, wasted energy, and inconsistent actuator performance across a production line. Pressure switch calibration is the controlled verification and adjustment of the pressure point where a switch changes electrical state. Done correctly, it protects equipment, stabilizes pneumatic performance, and gives maintenance teams confidence that a displayed or assumed pressure is actually the pressure controlling the machine.
For OEMs, integrators, and plant maintenance teams, the goal is not simply to make a switch trip at a number on its label. The goal is to confirm repeatable switching behavior under the real conditions of the application: rising pressure, falling pressure, expected load, correct electrical logic, and a reference instrument that can be trusted.
Why pressure switches drift in working equipment
Pressure switches operate in environments that are rarely ideal. Compressor vibration, pump pulsation, temperature cycling, airborne contaminants, moisture, and repeated diaphragm or piston movement gradually affect mechanical components. Contacts can wear or develop resistance. Springs can relax. Internal seals can harden, especially in applications with elevated temperatures or aggressive media.
The result is often drift, but drift is not the only failure mode. A switch may retain an accurate rising-pressure setpoint while its reset point moves outside tolerance. It may switch correctly during a bench check but chatter when installed near a pulsating pump. It may appear to be a pressure problem when the actual cause is voltage drop, a damaged connector, or a PLC input configured with the wrong logic.
This distinction matters. Adjusting a switch without diagnosing the system can hide the root cause and move a machine farther from its intended operating window.
Start with the control requirement, not the adjustment screw
Before connecting test equipment, confirm what the switch is intended to control. Is it a low-pressure alarm, compressor cut-in/cut-out function, vacuum confirmation signal, pump protection interlock, or process permissive? The answer defines whether the relevant value is the actuation point, reset point, or both.
A mechanical pressure switch commonly has a setpoint and differential. For example, a compressor pressure switch may open at 125 psi and close again at 100 psi. The 25 psi difference is the differential, sometimes called deadband. Some switches have a fixed differential; others allow independent adjustment. Changing the main setpoint on a fixed-differential design may shift both points together. On an adjustable-differential design, changing the differential can alter the reset point while leaving the cutout point nearly unchanged, depending on the mechanism.
Electronic pressure switches can add further variables: programmable hysteresis, normally open or normally closed output behavior, switching delay, window mode, and analog scaling. A calibration check must verify the programmed parameters as well as the actual process pressure. A perfectly accurate sensor with an incorrect hysteresis setting can still create poor machine behavior.
Equipment that supports a defensible calibration
The reference standard should be more accurate than the switch being tested. In most industrial work, use a recently calibrated digital pressure gauge or pressure calibrator with suitable range, resolution, and accuracy. A reference that is only marginally better than the pressure switch adds uncertainty instead of removing it.
Match the test source to the application. Clean, regulated shop air is appropriate for many pneumatic switches. A hand pressure pump provides controlled changes for hydraulic or higher-pressure units. Vacuum switches need a stable vacuum source and a reference capable of reading the applicable negative-pressure range. When testing refrigeration or process controls, use procedures and instruments compatible with the media and pressure range involved.
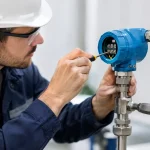
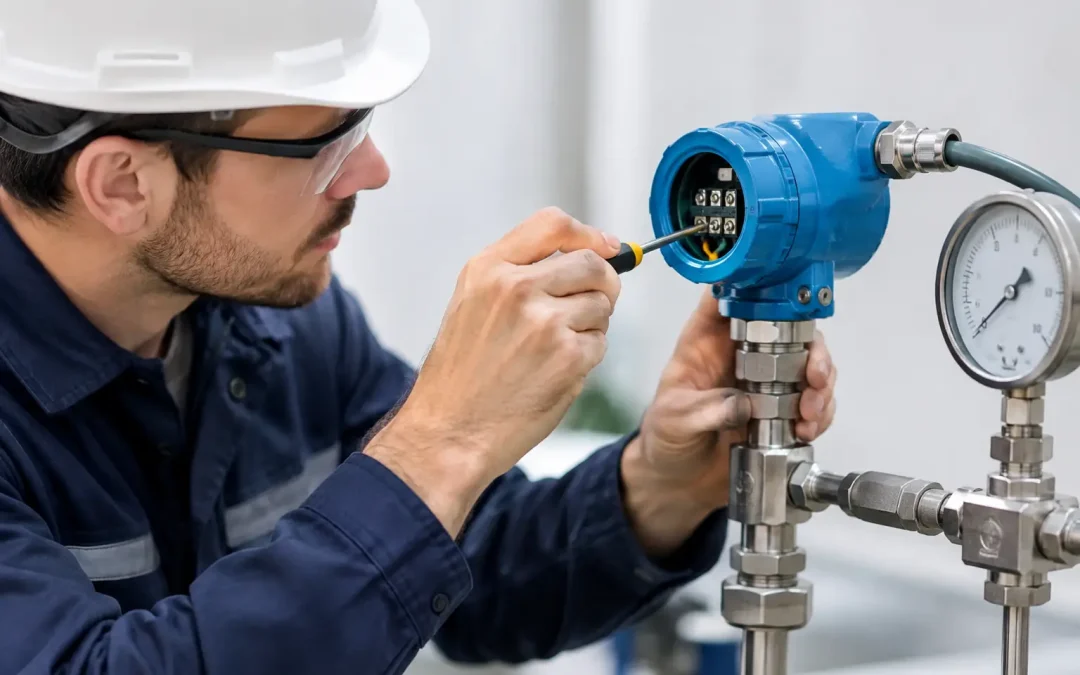
You also need a way to observe the electrical state. A multimeter set for continuity or voltage measurement is often sufficient for a dry-contact mechanical switch. For electronic switches, verify the supply voltage and measure or monitor the PNP, NPN, relay, or analog output as applicable. Confirm the wiring diagram before testing. A three-wire PNP switch and a dry-contact pressure switch do not validate the same way.
Pressure switch calibration procedure for field service
Isolate the switch from the operating process when possible, depressurize the connection safely, and apply the facility’s lockout/tagout procedure. If the switch serves a safety function, shutdown circuit, or pressure-relief protection strategy, do not alter settings without approved documentation and authorization.
Connect the reference gauge and the switch to the same controlled pressure source. Minimize restrictive fittings, leaking adapters, and long small-bore tubing that can delay pressure equalization. For pulsating systems, bench calibration is often more reliable than attempting to read a fluctuating gauge at the machine.
Increase pressure slowly toward the expected actuation point. Watch the reference pressure at the exact instant the electrical state changes, then record the rising-pressure value. Do not overshoot and estimate the point afterward. On a mechanical switch, repeat the rising test at least three times after allowing pressure to fall below the reset point between cycles.
Next, decrease pressure slowly and record the reset point. The difference between the rising and falling values is the actual differential. Compare both readings with the switch specification and the machine’s required operating limits. A switch can meet a broad catalog tolerance and still be unsuitable for a tightly controlled application, so acceptance criteria should come from the equipment design requirement whenever possible.
If adjustment is permitted, make small changes only. Return pressure below the reset point, repeat the rising and falling tests, and document every final value. Large adjustment turns are a common source of overshoot, particularly with compact mechanical switches where a small spring movement has a meaningful effect on the setpoint.
After bench verification, reinstall the switch, restore the system, and run an operational check. This final check confirms that the switch responds correctly to actual system pressure and that the control circuit interprets the signal properly.
Common calibration mistakes that create repeat failures
The most frequent mistake is relying on the machine gauge as the calibration reference. Panel gauges are useful for operation, but they may be damaged, poorly located, or inaccurate at the portion of the scale being used. A 0-200 psi gauge, for example, is a poor reference for verifying a 15 psi low-pressure alarm.
Another mistake is setting a pressure switch against a running compressor or pump without accounting for pressure pulsation. Pulsation can make contacts chatter and can cause a technician to chase a changing value. Install a properly sized snubber or use a stable test source when the application allows it. Do not add damping indiscriminately, however, because excessive restriction can slow response in a protection circuit.
Temperature also changes results. Mechanical switches calibrated in a cool maintenance area may respond differently near a hot process line or compressor discharge. If the process temperature is extreme, use a switch rated for that environment and consider remote mounting, a suitable isolator, or a pressure connection arrangement that protects the sensing element.
Finally, do not confuse calibration with compensation for a failing system. If pressure falls too quickly after shutdown, check for leaks, check valves, regulator creep, excessive air demand, or cylinder seal failures. Recalibrating the switch may stop an alarm temporarily while leaving the production problem untouched.
Selecting a switch that holds its setting
Calibration frequency depends on criticality, operating cycles, environment, and the consequences of a missed trip. A low-consequence utility air indication may require a periodic functional check. A switch protecting a pump from dry running, confirming vacuum for a robotic end effector, or controlling compressor loading deserves a documented interval based on risk and observed drift.
Component selection has a direct effect on calibration stability. Specify the appropriate pressure range rather than selecting an oversized range for every application. A switch operating near the center of its usable range generally provides more practical resolution than one forced to work at the extreme low end. Select wetted materials, electrical ratings, ingress protection, and vibration resistance for the actual installation, not the cleanest condition in the facility.
For demanding pneumatic and automation systems, VidoAir supports component selection with factory-direct access to pressure-control and air-preparation hardware designed for reliable industrial service. The right switch, installed with clean dry air and a stable pressure connection, reduces the amount of adjustment required later.
A calibration record should identify the switch tag, test date, reference instrument, rising setpoint, falling reset point, differential, technician, and any adjustment made. That record turns future troubleshooting from guesswork into trend analysis. When a switch begins moving out of tolerance, the best response is usually not another blind adjustment – it is a decision based on the application, the observed drift, and the cost of an unexpected stop.