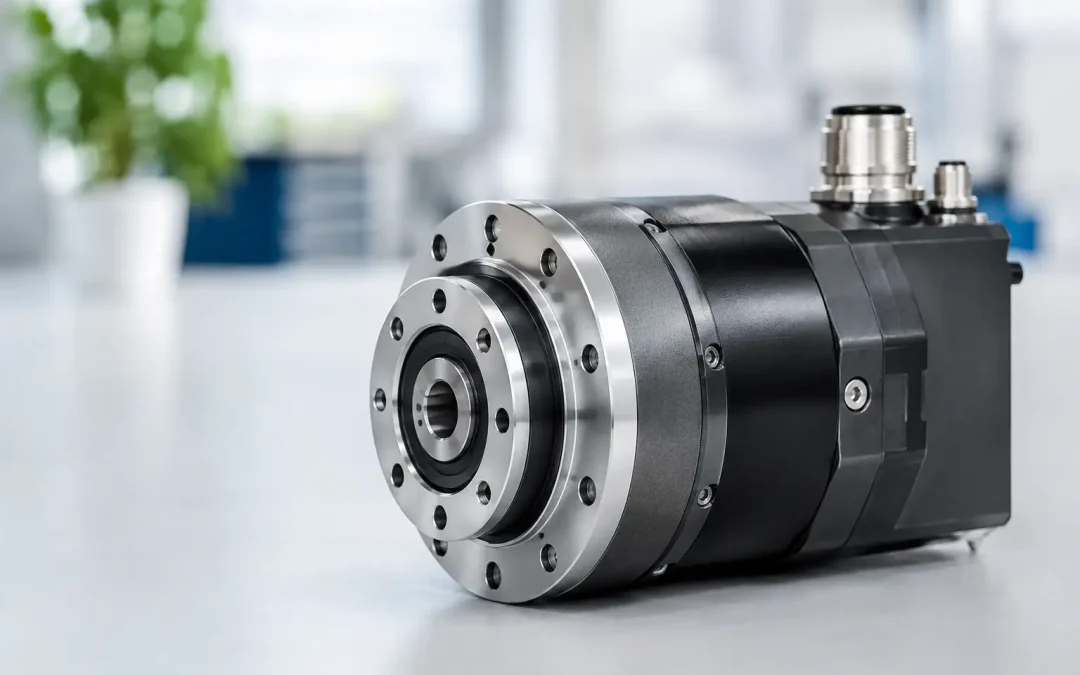
A rotary actuator can look correctly sized on a machine layout and still become the source of missed indexes, weak clamp positions, and inconsistent cycle times. The usual cause is not a defective component. It is a specification that focused on nominal torque while overlooking pressure variation, load inertia, external forces, cushioning, and the real duty cycle.
For OEMs, integrators, and maintenance teams, rotary actuators need to do more than turn a shaft. They must stop at the intended angle, resist the process load, survive repeated cycling, and fit into an air circuit that can supply enough flow at the point of use. Getting those details right reduces adjustment time and protects production uptime.
Start With the Load, Not the Bore Size
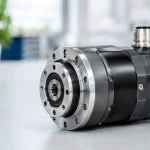
Pneumatic rotary actuators convert air pressure into angular motion through an internal rack-and-pinion or vane mechanism. Both designs can provide effective motion, but torque is not constant through every portion of the stroke in every design. Catalog torque values also assume a stated supply pressure, often with ideal flow conditions.
The first engineering question is whether the actuator has enough usable torque at the lowest pressure the machine will see. Plant header pressure is not necessarily actuator inlet pressure. Restrictions in filters, regulators, solenoid valves, fittings, tubing, and long runs can create a meaningful pressure drop when several devices cycle together.
Calculate the torque required to accelerate the load, overcome friction, and resist external forces. A rotating fixture, for example, may need torque for the fixture weight, a part being carried off-center, cable drag, seal friction, and process contact. If the load is vertical or overhung, gravity can add or subtract torque depending on actuator position. That means the worst case may occur at only one part of the rotation.
A practical safety factor is necessary, but it should not be used as a substitute for understanding the load. Oversizing an actuator can increase air consumption, impact energy, and mounting stress. Undersizing it causes sluggish motion, position drift under load, and premature internal wear. The right margin depends on how variable the load, pressure, and cycle demand will be.
Inertia Is Often the Hidden Problem
Torque starts motion, but inertia determines how difficult it is to accelerate and stop a rotating load. A lightweight part mounted far from the centerline can be more demanding than a heavier, compact load. Long arms, gripper tooling, and large-diameter nests deserve special attention because their mass is distributed away from the shaft.
When an actuator turns too quickly for its load, the result is often a hard end-of-rotation impact. Internal cushions can reduce that impact, but they are not a cure for excessive kinetic energy. Flow controls should be adjusted to control speed under actual production conditions, not only during an unloaded commissioning test.
If the process requires rapid indexing with a high-inertia load, assess whether a larger actuator, mechanical shock absorption, a shorter arm, or an alternative motion profile is needed. Pneumatic motion is highly effective for fast, repeatable transfer tasks, but it needs controlled energy management.
Choose the Rotary Actuator Design Around the Job
Rack-and-pinion rotary actuators are widely used for general automation because they offer compact packaging, practical torque capacity, and common angle options. Their output shaft arrangement makes them useful for diverters, stop gates, turning nests, indexing fixtures, and valve automation.
Vane-style rotary actuators can be a strong fit where compact geometry or a broad rotation range is required. However, available torque, internal sealing requirements, allowable side loads, and the nature of the stopping position should be reviewed carefully. The best design depends on the application rather than a universal preference.
For either style, identify whether the machine needs a simple end-to-end motion or multiple controlled positions. A standard double-acting pneumatic unit is efficient when the process only needs two repeatable positions. If the equipment must index through several angles, hold a mid-stroke station, or coordinate with inspection and robotics, the control strategy becomes more important.
Mechanical stops can establish repeatable end positions, while external sensors confirm that the actuator reached them. Adjustable stops provide flexibility during setup, but the adjustment mechanism must be secured after commissioning. A stop that drifts on a high-cycle machine quickly becomes a quality issue.
Build Position Feedback Into the Design
A rotary actuator can reach its mechanical stop without the control system knowing whether the required process condition occurred. For a noncritical diverter, that may be acceptable. For welding fixtures, part orientation, gating, or automated assembly, confirmation is usually worth the added hardware.
Magnetic piston sensing is common on pneumatic designs that support it. Proximity sensors can detect shaft or external flag positions where direct confirmation of rotation is needed. The sensor choice should reflect the machine environment: coolant, weld spatter, vibration, washdown, electrical noise, and cable routing can all affect field reliability.
Do not position sensors so close to a hard mechanical impact that vibration creates false transitions. Allow the actuator to settle before the PLC treats the position signal as a completed process step. This small timing decision can prevent intermittent faults that are difficult to reproduce during troubleshooting.
Air Circuit Details Decide Cycle Consistency
A high-performance actuator cannot compensate for an undersized valve or restricted air path. When a rotary motion is too slow, technicians often increase the regulator setting first. That can mask the real restriction while increasing impact at the end of travel.
Review valve flow capacity, tubing inside diameter, fitting restrictions, and exhaust path. Meter-out flow control is commonly preferred for pneumatic actuator speed control because it provides more stable movement as the load changes. The correct arrangement still depends on the direction of load and whether the application has an overrunning condition.
Air quality matters as much as flow. Water, compressor debris, degraded seals upstream, and incompatible lubricants can shorten service life. Use properly selected filtration and pressure regulation close enough to the actuator to maintain stable operating conditions. In washdown, food-adjacent, corrosive, or outdoor equipment, material selection and environmental protection deserve the same attention as torque calculations.
Troubleshoot Rotary Actuator Problems by Symptom
When a rotary actuator fails to complete travel, start by measuring pressure at the actuator inlet while it is moving. Static regulator pressure does not reveal a flow shortage. Then inspect the load for binding, tool interference, cable tension, and side loading on the output shaft.
If the unit reaches position but hits hard, reduce flow in a controlled way and verify cushion adjustment, if provided. Check whether the load changed after a tooling revision. A larger gripper, longer arm, or heavier workpiece may have increased inertia enough to overwhelm the original settings.
Inconsistent final angle can point to loose stops, wear in the fixture, shaft coupling backlash, contamination, or an actuator that is being asked to hold against a continuous external torque. Pneumatic actuators are excellent for positioning and clamping within their ratings, but a long-duration holding requirement may need a mechanical lock, brake, or different system architecture.
Air leakage is another frequent source of reduced performance. Listen for leakage around ports and valves, but also inspect tubing cuts, fitting engagement, and rodless or rotary seal areas where applicable. A slow leak can appear harmless until multiple axes cycle at once and the local pressure collapses.
Specify for Serviceability and Production Reality
The most effective specifications account for future maintenance. Confirm mounting dimensions, shaft interface, rotation angle, port size, sensor compatibility, and available replacement configuration before release. Standardizing these details across a machine family simplifies spares and reduces downtime when an actuator is damaged.
VidoAir supports pneumatic automation teams with factory-direct rotary actuator options, air preparation components, solenoids, fittings, tubing, and technical support for configured applications. Sourcing the motion device and its supporting air-control components with compatible performance targets helps eliminate avoidable integration gaps.
A rotary actuator should be treated as a controlled motion system, not an isolated catalog line item. When torque, inertia, air flow, sensing, stops, and service conditions are specified together, the result is predictable rotation that keeps pace with production instead of interrupting it.