A pneumatic valve bank that shifts correctly during bench testing can still create costly production faults once it is connected to a PLC panel. A mismatched output type, a shared common wired incorrectly, or an unprotected DC coil can produce erratic motion, damaged output cards, and difficult-to-trace downtime. Knowing how to configure PLC outputs means treating the logic, wiring, load characteristics, and commissioning process as one engineered system.
For OEMs, integrators, and maintenance teams, output configuration is not a software checkbox. It is the final control path between a machine decision and a physical action. Get that path right before startup, and solenoids, actuators, alarms, and interlocks behave predictably under real production conditions.
Start With the Output Device, Not the PLC Program
The correct PLC output configuration begins with the field load. Identify what the output must operate, its voltage, its steady-state current, its inrush current, its duty cycle, and whether it is inductive. A 24 VDC pneumatic solenoid coil, for example, is not electrically equivalent to a pilot light or a low-current relay input.
Document each point in an I/O schedule before assigning addresses. Include the device tag, function, supply voltage, normal state, output type, coil current, terminal number, and safety relationship. This gives engineering, panel build, controls, and maintenance teams one source of truth when troubleshooting later.
For pneumatic circuits, also define the intended fail state. A spring-return directional valve may de-energize to exhaust an actuator, while a double-solenoid valve may remain in its last commanded position. That difference affects not only PLC logic but also recovery behavior after a power loss, emergency stop, or controller restart.
Choose the Correct PLC Output Type
PLC output modules are commonly available as relay, transistor, and triac designs. The right choice depends on the load and operating environment, not simply on what is available in the panel.
Relay Outputs for Mixed Loads
Relay outputs use mechanical contacts and can switch AC or DC loads within their rated voltage and current limits. They are useful where a machine has mixed-voltage devices or where electrical isolation is required between the PLC electronics and the field circuit.
The trade-off is switching life. Relay contacts wear, can arc under inductive loads, and are not the best option for rapid cycling applications. A high-cycle pneumatic pick-and-place system may exceed the practical life of a relay output long before the mechanical equipment is due for service.
Transistor Outputs for 24 VDC Control
Transistor outputs are the standard choice for high-cycle 24 VDC automation loads such as solenoid valves, pneumatic manifolds, indicator lights, and interposing relays. They switch quickly, have no mechanical contact wear, and are well suited to demanding applications with frequent actuation.
Confirm whether the module is sourcing or sinking. A sourcing, or PNP, output supplies positive voltage to the load. A sinking, or NPN, output provides the return path to DC common. The field device and wiring scheme must match the output architecture. A PNP sensor and a sourcing PLC output can coexist in the same machine, but they are not wired to perform the same function.
For North American industrial control systems, PNP sourcing field devices are common. Still, never assume. Verify the electrical diagrams, module documentation, and actual terminal designations before connecting a load.
Triac Outputs for AC Loads
Triac outputs are designed for AC loads and are often used for contactors, AC solenoids, and small AC control devices. They are not suitable for DC loads. They also have leakage current and switching characteristics that can cause issues with very small loads or sensitive electronic devices.
If the application requires frequent switching, large inrush loads, or mixed supply voltages, an interposing relay or properly selected solid-state relay may be the better interface. It adds components, but it can protect an expensive PLC output module and simplify replacement during maintenance.
Size the Circuit for Real Load Current
A PLC output point rating is only one part of the decision. Check the rating per point, per common group, and for the entire module. Eight solenoids may each fall below the per-point limit but exceed the allowed current for their shared output common.
Inductive loads deserve extra attention. Solenoid coils, relay coils, contactor coils, and valve manifolds create a voltage spike when de-energized. That spike can damage transistor outputs, create electrical noise, or cause nearby inputs to change state unexpectedly.
Use the appropriate suppression method for the circuit. DC coils commonly use flyback diodes, transient voltage suppressors, or diode-resistor networks. AC coils may use RC snubbers or metal oxide varistors. The selection depends on required release speed. A basic flyback diode limits voltage effectively, but it can slow the release of a valve coil. For a high-speed pneumatic sequence, a TVS or engineered suppression device may offer a better balance between output protection and response time.
Place suppression close to the coil whenever practical. Protection installed several feet away at the panel may not control noise generated along a long field cable as effectively.
Wire Commons and Power Segments Deliberately
Output modules often group several channels under a common terminal. That common must be connected correctly for the module type. On a sourcing DC output module, the load is typically wired between the output terminal and DC negative. On a sinking module, the load is typically wired between DC positive and the output terminal.
Do not distribute all field loads from one unprotected supply branch merely because the PLC can address them individually. Segment power by machine zone or functional group, then protect each branch with appropriately sized fusing or electronic circuit protection. A shorted valve coil should not remove power from every output on a packaging line.
Separate control power from higher-noise loads where the design warrants it. Variable frequency drives, weld equipment, large contactors, and long motor leads can introduce electrical interference. Good grounding, shield termination where specified, cable separation, and clean DC power distribution improve output reliability far more than software changes made after the fact.
Configure Logic for Safe, Observable Machine Behavior
In the PLC program, use descriptive tags that identify the field device and its action. `Clamp_Extend_Solenoid` is more useful during troubleshooting than `Output_17`. Pair the command bit with feedback where the machine design supports it. A commanded cylinder extension without a corresponding end-of-stroke sensor within the required time should create a controlled fault, not allow the sequence to continue.
Avoid driving physical outputs directly from complex sequence logic when possible. A layered approach is easier to diagnose: sequence logic requests an action, permissives validate that the action is allowed, and an output routine drives the final point. This structure makes it clear whether a valve failed because the PLC never requested it, an interlock blocked it, or the output circuit did not energize.
For outputs that must default off after a restart, explicitly initialize command bits and prevent automatic motion until the machine is in a verified ready state. This matters especially for double-solenoid pneumatic valves, conveyor controls, and gripper circuits where retained logic states could command unexpected movement after a power interruption.
Test Every Output Before Full-Speed Production
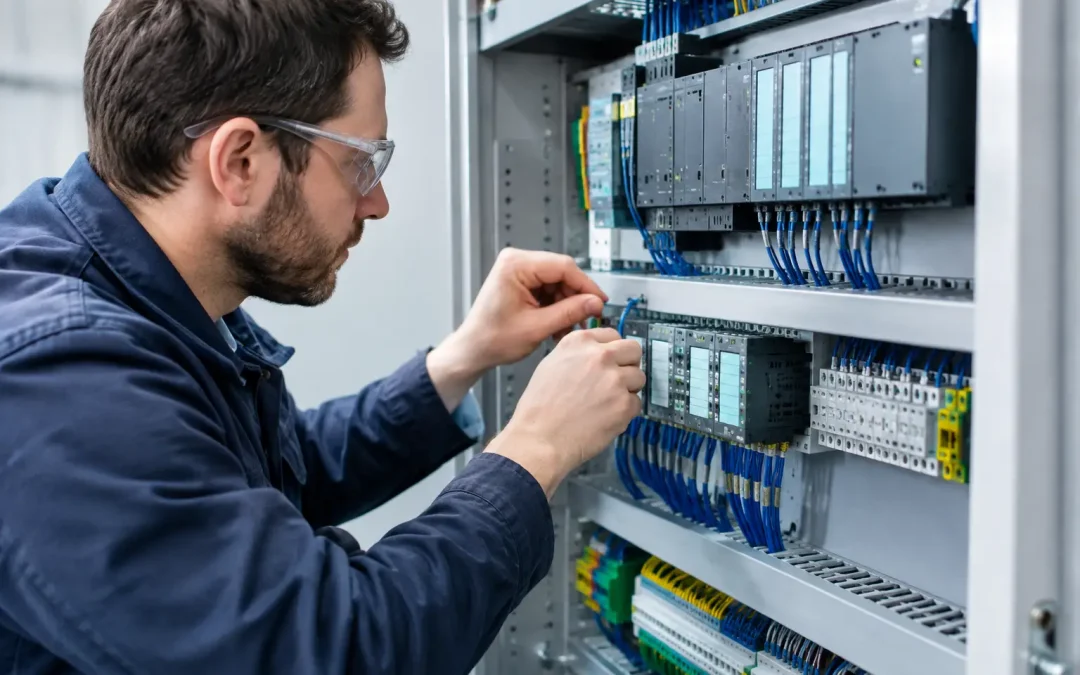
Commissioning should move from the terminal outward. First, verify the correct field supply voltage and polarity with a meter. Then force or command one output at a time according to approved safety procedures. Confirm the output LED, voltage at the module terminal, voltage across the load, and actual device response.
If an output LED turns on but a solenoid does not shift, do not immediately replace the valve. Check for an open coil, incorrect common wiring, a blown branch fuse, voltage drop under load, or a connector issue. If voltage is present at the coil but the actuator still does not move, the problem may be pneumatic: insufficient pressure, a blocked exhaust, a manually overridden valve, or a mechanically bound cylinder.
Record final measured current for critical output groups. This baseline is valuable later. A coil that begins drawing abnormal current or a manifold circuit with declining voltage under load can be identified before it becomes an unplanned shutdown.
Common PLC Output Failures and Their Root Causes
The fastest troubleshooting comes from separating logic faults from electrical faults. Start by asking whether the controller is commanding the output. If the command is absent, inspect interlocks, sequence state, safety conditions, and communication health. If the command is present but the physical device is inactive, follow the circuit from output terminal to load.
Repeatedly failed transistor channels often point to inadequate coil suppression, excessive inrush current, or incorrect wiring. Outputs that work intermittently may indicate loose terminals, undersized conductors, voltage drop, contaminated connectors, or a marginal power supply. A valve that remains energized when it should release may be caused by a welded relay contact, leaked current from an AC output, a program latch, or the mechanical behavior of a detented valve.
Treat output failures as system evidence rather than isolated component defects. Replacing a module without correcting the load condition usually moves the failure to the next channel.
A well-configured PLC output circuit gives maintenance teams a clear path from command to motion and gives production a machine that behaves consistently under load. Build that clarity into the design, measure it during commissioning, and document it at the panel – the next troubleshooting call will be shorter because of it.