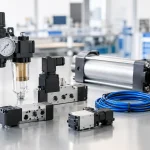
A pneumatic cylinder that hesitates at the end of a packaging cycle is rarely a mystery for long. The valve may be mechanically sound, air supply may be adequate, and the PLC may show its output command as active. Yet the coil never receives enough usable power to shift the spool. Can PLCs control solenoid valves? Yes, and they do so in virtually every modern automated machine. The real engineering question is whether the PLC output, valve coil, wiring method, and control logic are matched well enough to deliver repeatable motion under production conditions.
For straightforward applications, a PLC can command a 24 VDC solenoid valve directly. For larger valve banks, higher-current coils, AC coils, or systems that need electrical isolation and easier field replacement, an interposing relay or remote output module is often the better design. Choosing between those approaches affects cycle consistency, output life, troubleshooting time, and downtime risk.
Can PLCs Control Solenoid Valves Directly?
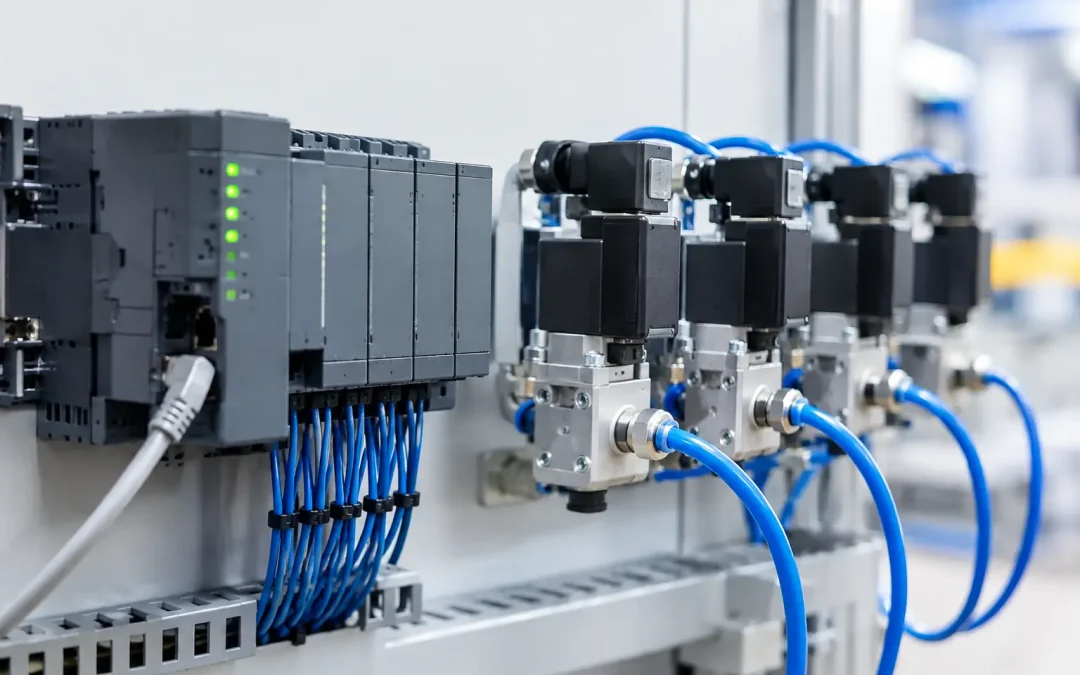
A PLC does not control compressed air itself. It switches an electrical signal to a solenoid coil, and the energized coil shifts a valve spool or poppet. That valve then routes air to an actuator, gripper, slide table, vacuum generator, or another pneumatic device.
Most PLC transistor outputs are designed for 24 VDC loads, which makes them a natural fit for common DC pneumatic valve coils. A sourcing output provides positive voltage to the load, while a sinking output completes the path to 0 V. The coil and PLC wiring must match the output type. This is basic, but sourcing-versus-sinking mismatches remain a common startup failure when equipment, replacement valves, and field wiring come from different standards.
Direct control works best when the coil’s steady-state current and inrush current are comfortably within the PLC output rating. The coil data sheet may list power in watts rather than current. For a 24 VDC, 2.5 W coil, current is approximately 0.10 A. That appears small against a 0.5 A output rating, but output selection cannot stop there. Engineers also need to account for each output channel, the total current per output group or common, power supply capacity, ambient heat, and the effect of inductive switching on the output electronics.
A PLC output should not be specified at its absolute maximum simply because calculations say it will survive. Production equipment needs margin. A valve island cycling across multiple stations, particularly in a warm enclosure, can expose weaknesses that a bench test will not reveal.
Direct output control is usually appropriate when
Direct PLC control is typically a sound choice for 24 VDC coils with low current draw, short and protected cable runs, and outputs rated for inductive loads. It also suits compact machines where minimizing panel hardware matters and the PLC has enough spare I/O for future changes.
The trade-off is that a failed shorted coil, wiring fault, or repeated transient event can damage an output point or an entire output group. Replacing a PLC module is more disruptive and more expensive than replacing a relay interface. For a low-risk valve or a carefully protected valve manifold, that trade-off may be acceptable. For a critical machine zone, it may not be.
Start With Coil and Output Data, Not the Valve Symbol
The pneumatic schematic shows function. The electrical data determines whether the PLC can operate the valve safely. Before finalizing the circuit, verify coil voltage, DC or AC supply, wattage or current draw, inrush behavior, duty rating, connector type, and any integral suppression or indicator circuitry.
DC coils are generally the simplest choice for PLC-operated pneumatic valves. They pair directly with standard 24 VDC control systems and allow fast, repeatable switching. AC coils can be useful in legacy installations or specific plant standards, but they normally require an appropriately rated relay, contactor, solid-state interface, or PLC output module designed for AC loads. A standard DC transistor output cannot switch an AC solenoid coil directly.
Also distinguish between a single-solenoid, spring-return valve and a double-solenoid valve. A spring-return valve needs power only to shift into its actuated position, then returns when the command is removed. A double-solenoid valve can hold its last shifted state after power is removed. That behavior changes both the control program and the machine’s response to an emergency stop, power loss, or fault reset.
For safety-related motion, do not assume that de-energizing a normal process valve creates a safe condition. The correct architecture depends on the hazard assessment and may require monitored safety valves, dump circuits, controlled exhaust, mechanical stops, or other protective measures. A standard PLC output is not a safety function unless the complete system has been designed and validated for that role.
Wiring Practices That Protect PLC Outputs
Solenoid coils are inductive loads. When the PLC turns a DC coil off, the collapsing magnetic field produces a voltage spike. Without a controlled path for that energy, the transient can stress transistor outputs, interfere with nearby signals, and contribute to premature failures.
Use suppression appropriate to the application. A flyback diode across a DC coil is effective and inexpensive, but it slows coil release because current decays gradually. That can be unacceptable on fast pneumatic sequences, especially where cylinder timing, vacuum release, or high-speed sorting depends on rapid valve de-energization. A diode plus Zener, transient voltage suppressor, or dedicated surge suppressor can allow quicker release while still limiting damaging voltage. The correct choice is a timing decision as much as a protection decision.
Keep coil wiring separate from low-level analog and communication wiring wherever practical. Use adequately sized conductors for the run length and total load, terminate shielding correctly where shielded cable is used, and label every valve output at the panel and manifold. Good labeling sounds administrative until a technician must isolate one failed coil from a 24-station valve bank during a night shift.
A fused or electronically protected 24 VDC valve supply is equally valuable. It prevents one damaged cable or failed coil from taking down all machine outputs. Segmenting valve banks by machine zone can reduce the fault impact further and makes troubleshooting more direct.
Use Interposing Relays and Remote I/O Where They Add Value
An interposing relay places a replaceable interface between the PLC and the solenoid coil. The PLC energizes the relay coil, and the relay contact switches the valve supply. This arrangement is useful when the valve load exceeds PLC output capability, when switching AC coils, or when electrical isolation is required.
Relays are not automatically better. Mechanical contacts wear, contact bounce can matter in specialized circuits, and relay panels consume space. For high-cycle applications, a quality solid-state interface or a remote transistor output module may offer longer service life and cleaner diagnostics. The right answer depends on cycle rate, load type, maintenance strategy, and the consequences of an output failure.
Remote I/O is often the better architecture for distributed machinery. Locating an IP-rated valve manifold and output block close to the actuators reduces long cable runs, simplifies installation, and improves fault visibility. When the network and diagnostics are specified correctly, technicians can identify a missing output command, blown channel protection, or manifold communication issue without tracing every conductor back to a central cabinet.
PLC Logic Should Confirm Motion, Not Just Command It
A PLC output bit only confirms that the program requested a solenoid to energize. It does not prove the valve shifted, air reached the actuator, or the mechanism completed its motion. Treating an output command as proof of action is a frequent source of intermittent machine faults.
Use end-of-stroke sensors, pressure switches, vacuum switches, or position feedback to verify the expected result. A cylinder extend routine, for example, should energize the extend solenoid and start a timer. If the extended sensor does not arrive within the allowed window, the PLC should alarm with useful context: valve command active, expected sensor missing, and station identification.
This diagnostic approach separates electrical and pneumatic faults quickly. If the output command is absent, investigate logic permissions, interlocks, and I/O mapping. If the output is present but the coil is not energized, test supply voltage, fusing, wiring, and the output device. If the coil is energized but motion does not occur, investigate air pressure, valve spool contamination, exhaust restrictions, actuator binding, and mechanical load.
Avoid rapidly toggling a valve output in an attempt to overcome poor motion. Repeated chatter can overheat coils, accelerate spool wear, and hide the underlying issue. If a valve requires repeated commands to move an actuator, the system needs inspection, not a louder software command.
Design the Valve Circuit for the Production Floor
The strongest PLC-to-solenoid design is not merely one that works at commissioning. It remains predictable when voltage drops during simultaneous actuation, when an operator replaces a coil, when a cable is damaged, and when a technician needs to isolate a fault under time pressure.
Specify coil voltage and output capacity with margin, use suppression that fits the required release time, protect valve power by zone, and build feedback into every motion where confirmation matters. Match the pneumatic valve’s fail state to the machine’s operating and safety requirements before the PLC program is written.
For engineered pneumatic assemblies, VidoAir can help align valve, coil, actuator, air preparation, and control hardware around the actual duty cycle rather than a nominal catalog rating. That is where reliable automation is won: at the point where electrical switching, air flow, and mechanical motion are designed as one system.